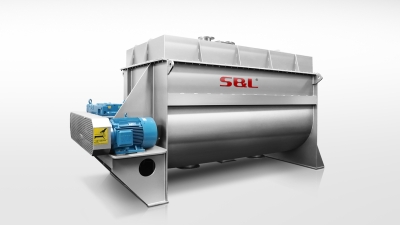
In the fast-changing world of pharmaceutical manufacturing, everyone’s really focused on making processes more efficient and consistent. A recent report from the International Society for Pharmaceutical Engineering (ISPE) shows that over 70% of pharma companies are keen on adopting advanced mixing tech to boost product quality and make operations run smoother. Among all those options, the Cone Mixer really catches the eye — it’s super versatile and innovative, providing impressive blending power to ensure everything’s uniform. Here at Shuanglong Group Co., Ltd., we’re proud to offer cutting-edge mixing solutions designed specifically to meet the tough standards of the pharma industry. With a passionate team of over 150 experts based in our Shanghai factory, we combine the latest technology with hands-on support. We’re fully committed to delivering reliable, efficient solutions, and we see ourselves as a trusted partner in the journey toward excellence in mixing technology.
Key Advantages of Cone Mixers in Pharmaceutical Production
Cone mixers are pretty essential in pharmaceutical manufacturing, mainly because their unique design helps improve both accuracy and efficiency when blending powdery ingredients. Their cone shape isn’t just for looks—it actually helps create a more uniform mix, which means less chance of ingredients separating during the process. That’s especially important in pharma, where making sure things are mixed evenly can really impact how well the final product works. Plus, these mixers make it easier for materials to flow smoothly, which can really speed up production and cut down on hassle.
One of the best things about cone mixers is how versatile they are. They can be tailored to different production sizes, whether you're making small batches or large quantities—no problem. This kind of flexibility is a lifesaver in pharma, where formulations and volumes tend to vary a lot. They also work really well with more advanced continuous mixing tech, so companies can keep productivity high without sacrificing quality.
Pro tip: When you're picking out a cone mixer for pharma work, think about your specific needs—things like particle size and moisture levels matter. Using tools like Discrete Element Method (DEM) simulations can give you a heads-up on how well your mixer will perform, helping you fine-tune your process. And, of course, always go for equipment that ticks all the regulatory boxes—quality and safety are non-negotiable here.
Enhancing Efficiency in Drug Formulation with Cone Mixers
You know, in the pharma world, trying to make drug formulation more efficient never really stops, right? One of the cool innovations that’s been gaining attention is cone mixers. These little devices might seem simple, but they’re pretty essential for getting powders to blend just right—smooth, even, and consistent. The design of cone mixers is pretty clever; they’re gentle enough not to damage sensitive ingredients, yet effective at mixing everything uniformly. It’s like they know just how to do the job without a fuss.
On top of that, they really help speed things up. Traditional mixing methods can be pretty time-consuming, but cone mixers cut down on that quite a bit. They can handle all sorts of materials—powders, granules—you name it—which makes them super flexible for different manufacturing needs. Plus, because they can run continuously, they’re perfect for streamlining production. Manufacturers can even monitor and tweak the process on the fly, which means faster turnaround times for new drugs without sacrificing quality. All in all, they’re a pretty handy tool in the pharma toolkit, helping get medicines to market quicker and better than ever before.
Innovative Uses of Cone Mixer in Pharmaceutical Manufacturing Processes - Enhancing Efficiency in Drug Formulation with Cone Mixers
| Application | Benefits | Efficiency Improvement | Process Time Reduction |
| Uniform Powder Blending | Enhanced consistency in formulations | Up to 30% faster blending | Reduced by 10 minutes per batch |
| Granulation Processes | Improved particle size distribution | 15% increase in yield | Speed up by 5 minutes |
| Dry Blending | Expedited mixing process | 25% less energy consumption | Time reduced by 8 minutes |
| API and Excipients Mixing | Consistent drug potency | Improved batch homogeneity | Less than 15 minutes per batch |
| Coating Formulations | Better coating adhesion | 20% faster process | Reduced by 12 minutes |
Improving Product Consistency through Advanced Mixing Techniques
You know, in the pharmaceutical world, making sure each product is consistent is a big deal—it's key to making sure everything works well and stays safe. Among all the tools out there, the cone mixer really catches the eye because of its clever design and super effective mixing abilities. It does a great job of blending powders and granules smoothly, which means the final product ticks all the boxes for uniformity. The cone shape? It’s pretty genius—it’s gentle but still gets the job done, helping to evenly distribute particles, which is so important when putting together medicines.
And here's the cool part: the cone mixer gives manufacturers a lot of control over the process. You can tweak things like mixing time, speed, or even humidity to match the specific formulation you’re working on. That kind of flexibility means results are more consistent every time. By using these high-tech mixing methods, the cone mixer doesn’t just improve the quality but also cuts down on the chances of batch-to-batch variation. Basically, it helps pharma companies produce more reliable products, which means better quality and more trust from folks who take these meds every day.
Minimizing Contamination Risks in Pharmaceutical Mixing Processes
In the world of pharmaceutical manufacturing, avoiding contamination is basically a non-negotiable if you wanna make sure your products are safe and effective. Newer tech, like cone mixers, really helps with that. They create a pretty controlled environment, which means less risk of exposing the ingredients to contaminants while mixing. Plus, their design ensures everything gets blended evenly without worrying about cross-contamination—making them especially great for sensitive ingredients that need a gentle touch.
On top of that, there’s been a big push towards aseptic processing, which is all about cutting down human handling that could introduce germs or errors. Using automated mixers and single-use systems makes a difference here. They help reduce mistakes and speed up things at the same time. All these smart innovations don’t just make production smoother—they also help keep everything super clean and safe. In the end, they help manufacturers deliver products that meet those strict quality standards we all expect.
Cost-Effective Solutions: Cone Mixers Vs. Traditional Equipment
When it comes to making pharmaceuticals, keeping costs under control is a big deal. That’s where cone mixers really shine—they’re often seen as a strong alternative to the traditional mixing stuff. According to a report by Mordor Intelligence, the global market for pharmaceutical mixing equipment is expected to grow at around 5.2% annually between 2021 and 2026. This growth is mainly fueled by the increasing need for efficient and reliable mixing processes. Cone mixers, in particular, are great because they gently blend ingredients without overdoing it, which helps prevent product degradation—something that high-shear mixers can sometimes cause. That means better quality end products and less waste, which is pretty awesome.
Plus, these mixers can save a ton on operational costs and energy. Research published in the International Journal of Pharmaceutics shows that using cone mixers often requires about 30% less energythan traditional ribbon or Paddle Mixers. That’s a pretty significant saving, especially when it comes to utility bills. For manufacturers trying to tighten up their budgets, that can make a big difference. Overall, switching to cone mixers isn’t just good for product quality—it’s also a smart move forsustainability since they cut down on energy use and waste overall.
The Role of Cone Mixers in Meeting Regulatory Standards in Pharma
In the pharmaceutical industry, things are about as regulated as they come, so making sure that every product is consistent and uniform really isn't optional—it's everything. That's where cone mixers come in; they’re pretty much essential because of their unique design and how they work. The cone shape helps mix everything thoroughly and also reduces the chances of separation when you unload the materials, which is super important for meeting all those strict rules and standards. Lately, researchers have been stressing how crucial it is to get unloading just right—any little segregation during that step can throw things off, so the mixer’s role becomes even more critical in keeping the quality top-notch.
On top of that, using cone mixers can actually help companies stick to Good Manufacturing Practices, or GMP for short. They make controlling the mixing process easier, leading to more uniform blends that meet the demanding testing requirements set by regulators. As pharma makers keep pushing to improve, adopt new standards, and refine their processes, incorporating advanced tech like cone mixers is becoming more and more important. Not only does this make production smoother, but it also boosts the safety and effectiveness of the medicines we rely on—in the end, that’s good news for both the manufacturers and the people who count on these products every day.
Exploring the Efficiency of Horizontal Ribbon Mixers: Insights from the Latest Industry Reports and Data
Horizontal Ribbon Mixers are pivotal in achieving efficient and uniform mixing of various materials, making them indispensable across numerous industries. The latest industry reports highlight their effectiveness, particularly due to their traditional double ribbon design, which promotes gentle mixing. This feature is crucial for heat-sensitive materials, ensuring that the integrity and quality of the products are maintained during processing.
Furthermore, the versatility of Horizontal Ribbon Mixers is evident in their wide range of flexible capacities. Whether in a facility with limited height or in need of extra-large sizes to handle mature production demands, these mixers can be tailored to fit specific operational needs. The paddle-style and discontinuous ribbon designs contribute to their performance, allowing for a more thorough mix while minimizing material degradation. By investing in a Horizontal Ribbon Mixer, industries can leverage these insights to enhance their mixing processes and ultimately improve product quality.
FAQS
: Cone mixers enhance precision and efficiency in blending powdered substances, leading to a more homogeneous mixture and reducing the risk of segregation.
Their conical shape facilitates better flow, which can significantly streamline production processes in pharmaceutical manufacturing.
Yes, cone mixers are adaptable and can be customized to accommodate both small and large batch sizes, making them suitable for various formulations.
Cone mixers efficiently integrate with advanced continuous mixing technologies, ensuring high productivity while maintaining quality standards.
It is important to consider the specific requirements of your formulation, including particle size and moisture content.
DEM simulations provide valuable insights into mixing performance, which can help optimize the mixing process.
Yes, cone mixers are a competitive alternative that offers significant savings in operational costs and energy consumption.
By minimizing the risk of product degradation, cone mixers ensure higher-quality end products compared to high-shear mixers.
Cone-type mixers often require 30% less energy than traditional mixers, contributing to lower utility bills.
They reduce energy consumption and overall waste, helping manufacturers align their processes with sustainability objectives.
Conclusion
In our blog, 'Innovative Uses of Cone Mixers in Pharmaceutical Manufacturing,' we really dive into how these mixers play a crucial role in making the pharma production process smoother and more reliable. They’re great for boosting efficiency and ensuring that each batch of medication comes out consistent—that’s a big deal in this industry! Plus, they help streamline the drug formulation process and cut down on contamination risks, which is always a plus. And honestly, compared to older, traditional equipment, cone mixers can be a more budget-friendly option, making them a pretty valuable tool for manufacturers looking to stay ahead.
Here at Shuanglong Group Co., Ltd., we take pride in offering equipment that hits the mark when it comes to performance and dependability. Our cone mixers don’t just help pharma companies stay compliant with regulations—they also use cutting-edge mixing techniques to help optimize production and get better results. With a passionate team of over 150 folks working at our Shanghai facility, we’re dedicated to being your go-to partner for innovative mixing solutions. We’re all about supporting your success with reliable, top-notch equipment and expert assistance.